Explore our elite collection of engineered protective solutions crafted for supreme durability, aesthetics, and global optical retail standards.
Rigorous analytical insights into Danyang’s global optical cluster and strategic manufacturing framework adhering to top-tier E-E-A-T standards.
As we all know, Danyang is a well-known national eyewear production, sales, service distribution center, the glasses industry entity production industry foundation is strong, the market scale is large. Operating from this thriving metropolitan hub, Danyang River Optical Glasses Co., Ltd. has established itself as an indispensable nexus for comprehensive eyewear accessories, precision spectacle frames, high-clarity lenses, advanced optical equipment, and specialized contact lenses.
Rooted deeply within the Danyang glasses marketplace, our firm serves national and international eyewear industry retailers with unyielding dedication. By strategically integrating offline manufacturing powerhouse assets located within China's largest optical base, we maintain exceptional proximity to major logistical networks including the Shanghai-Nanjing Expressway, Shanghai Pudong International Airport, Nanjing Lukou International Airport, and Changzhou Airport. This strategic deployment ensures lightning-fast dispatch, streamlined inventory turns, and optimized supply chain elasticity.
Established on March 12, 2012, our organization has maintained a continuous trajectory of innovation, scaling our operations to forge an elite, professional online optical B2B procurement portal tailored exclusively for modern optical retailers.
Company Vision: To provide one-stop shopping and service easier. We leverage advanced digital architecture to strip away traditional multi-layered distribution inefficiencies.
Company Value: To become a one-stop procurement and service center. We commit to absolute transparency, stringent quality verification, and uncompromised commercial reliability.
Company Spirit: Unity and hard work, perseverance, self-pressure, dare to compete. This internal ethos drives our engineering teams and quality auditors to push past standard industry benchmarks.
Rapid social development, iterative update of science and technology, with the advent of the 5G Internet era, the entire business system is undergoing earth-shaking changes. The traditional offline optical mall business model faces unprecedented paradigm challenges. To serve optical industry retailers with maximum agility, we engineered a comprehensive, data-driven one-stop online procurement ecosystem.
The platform operates on 4 core functional pillars: precision garage lens customization engines, data-driven optical store marketing paired with professional technical training, exclusive VIP membership tier services, and advanced private domain traffic promotion mechanisms. Our catalog extensively covers 6 primary product categories: optical lenses, optical frames, premium sunglasses, contact lenses, clinical optical equipment, and specialized accessories/consumables.
Furthermore, our infrastructure highlights 8 core competitive advantages: complete diversification of optical goods, infallible product quality assurance, real-time online order fulfillment tracking, premium after-sales support, worry-free hassle-free returns, aggregation of internationally renowned brands, ultra-convenient high-efficiency procurement, and distinct direct-factory price advantages. Backed by independent internal software engineering units and rigorous quality control inspection squads, we govern raw material sourcing, safety compliance, and finishing supervision with zero-tolerance protocols. This effectively alleviates retail overstock burdens and reshapes global optical procurement paradigms.
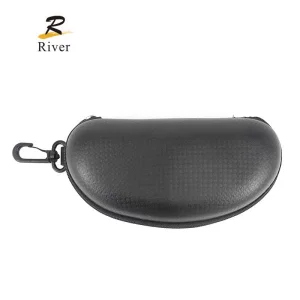
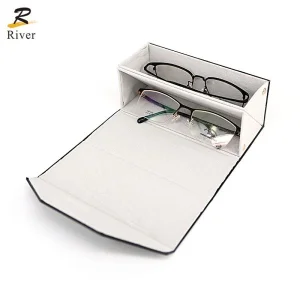
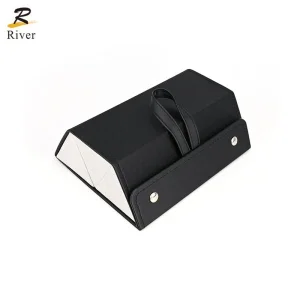
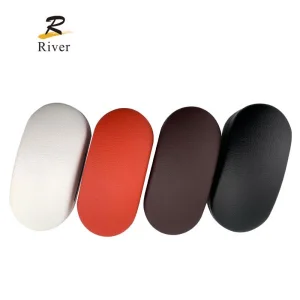
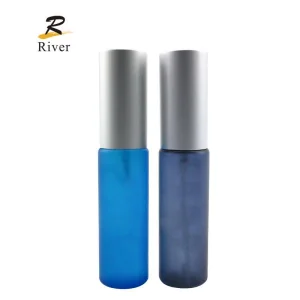
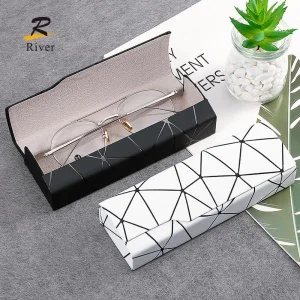
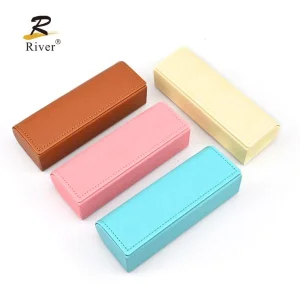
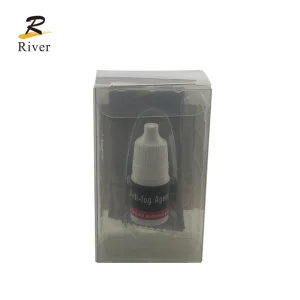
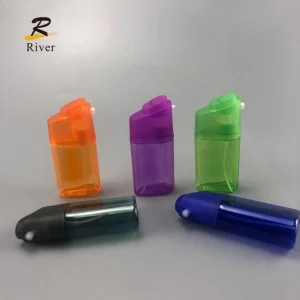
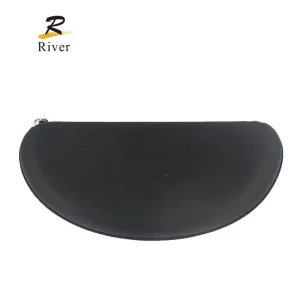
1. Protective Consumables & Accessories: Advanced anti-fog/quick-clean lens sprays (e.g., LC038, LC024, LC306), ultra-fine microfiber cleaning cloths, hardshell/semi-hard EVA cases, custom handmade leather pouches, delicate tissue wipes, and branded retail paper bags.
2. Precision Eyewear Hardware & Tools: Eyewear chains, optical pliers, micro-screwdrivers, medical-grade silicone nose pads, blocking pads, and ergonomic anti-slip temple hooks.
3. Advanced Optical Equipment: Industry-leading diagnostic and processing units from Topcon, Essilor, Nidek, Tianle, Xianyuan, and Jinggong.
4. Designer & Independent Frames: BOSS, Jimmy Choo, Bai Nianhong, Chnkeluoxin, Playboy, Pengke, Kiss My Mudoo, and Excellandun.
5. High-Performance Lenses & Contact Lenses: Global optical standards featuring Essilor, Zeiss, Hoya, Synchrony, Chemi, Alcon, Bausch + Lomb, Hydron, Horien, and CooperVision.
Discover specialized cleaning formulations, premium EVA cases, and high-performance ergonomic accessories designed for ultimate clarity and protection.
An authoritative breakdown of localization scenarios, future engineering roadmaps, and international compliance standards for custom sunglasses belt cases.
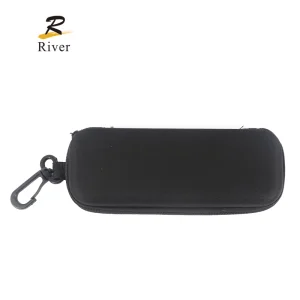
The utility of a specialized custom sunglasses belt case transcends basic physical protection; it represents an active lifestyle accessory integrated into modern urban commuting, extreme outdoor sports, and luxury retail merchandising. In metropolitan environments across North America and Western Europe, consumers demand modular belt-attachment mechanisms that allow instant, hands-free accessibility during cycling, hiking, and daily transit.
By engineering high-density EVA cores wrapped in abrasion-resistant PU leather or ballistic nylon, our manufacturing lines ensure that sunglasses remain entirely secure against high-impact compression while hanging securely from tactical or casual belts. Retailers deploying localized merchandising displays benefit significantly from custom-embossed branding options, which turn utilitarian protective cases into powerful wearable marketing assets.
As smart eyewear and augmented reality (AR) glasses gain mainstream commercial traction, the packaging industry faces an urgent evolutionary mandate. Our R&D division is actively spearheading the next generation of smart-storage solutions. Future trajectories include:
1. Biodegradable Composite Materials: Transitioning from traditional petrochemical EVA polymers to bio-based, closed-cell foams that reduce carbon footprints without compromising shock-absorption integrity.
2. RFID & NFC Integrated Tracking: Embedding micro-chips within case linings for high-end luxury authentication and loss-prevention tracking.
3. Advanced Thermal & Moisture Regulation: Incorporating micro-ventilation channels and anti-microbial interior velvet linings to safeguard delicate polarized coatings against extreme climatic shifts.
The manufacturing prowess concentrated in Danyang, Jiangsu Province, represents an unparalleled benchmark of supply chain resilience. Unlike decentralized manufacturing frameworks prone to logistical bottlenecks, our regional cluster houses a fully closed-loop ecosystem—from raw chemical foam compounding and precision metal stamping for zippers to automated laser-cutting and eco-friendly screen printing.
This localized vertical integration eliminates unnecessary intermediate freight costs and slashes production lead times by up to 40%. Global B2B buyers partnering with our direct-factory infrastructure gain immediate access to scalable mass-production capabilities, stringent ISO-certified quality assurance gates, and aggressive tiered wholesale pricing models that maximize commercial profitability.
Navigating international regulatory requirements is vital for smooth cross-border B2B distribution. Our manufacturing protocols strictly adhere to global compliance mandates, including REACH (Registration, Evaluation, Authorisation and Restriction of Chemicals) standards for the European market and CPSIA (Consumer Product Safety Improvement Act) regulations for North America.
Every batch of custom sunglasses belt cases undergoes rigorous stress testing—including zipper fatigue cycles, drop-impact absorption assays, and chemical migration screening for heavy metals and phthalates. This unwavering commitment to safety and compliance establishes absolute trust between our factory floor and global optical retail chains.
Q1: What is the standard minimum order quantity (MOQ) for custom-branded sunglasses belt cases?
A: To support growing optical brands and established retail chains, we offer flexible MOQ structures starting from 500 units per custom color and logo design, utilizing our in-house mold tooling capabilities for rapid prototyping.
Q2: Can we request custom interior layouts to fit oversized or wrap-around sports sunglasses?
A: Absolutely. Our engineering team utilizes CAD-guided thermoforming molds to custom-engineer internal cavities tailored precisely to your specific frame geometries.
Q3: What are the typical lead times for sample development versus mass production?
A: Digital 3D renderings and physical sample prototypes are typically finalized and dispatched within 5 to 7 business days. Mass production runs are completed within 15 to 25 days depending on total order volume.